Understanding How a ZLD Plant Works
A Zero Liquid Discharge (ZLD) plant is an integrated industrial wastewater treatment system designed to recover water while concentrating the dissolved contaminants that remain in the wastewater for appropriate final management. Unlike conventional wastewater treatment systems, a ZLD process is designed to minimize or eliminate the final discharge of wastewater as a liquid stream.
Understanding how a ZLD plant works starts with one basic principle: water is progressively separated from dissolved and suspended contaminants through multiple treatment stages. Depending on the wastewater characteristics, these stages can include pre-treatment, reverse osmosis, evaporation, concentration, drying and crystallization.
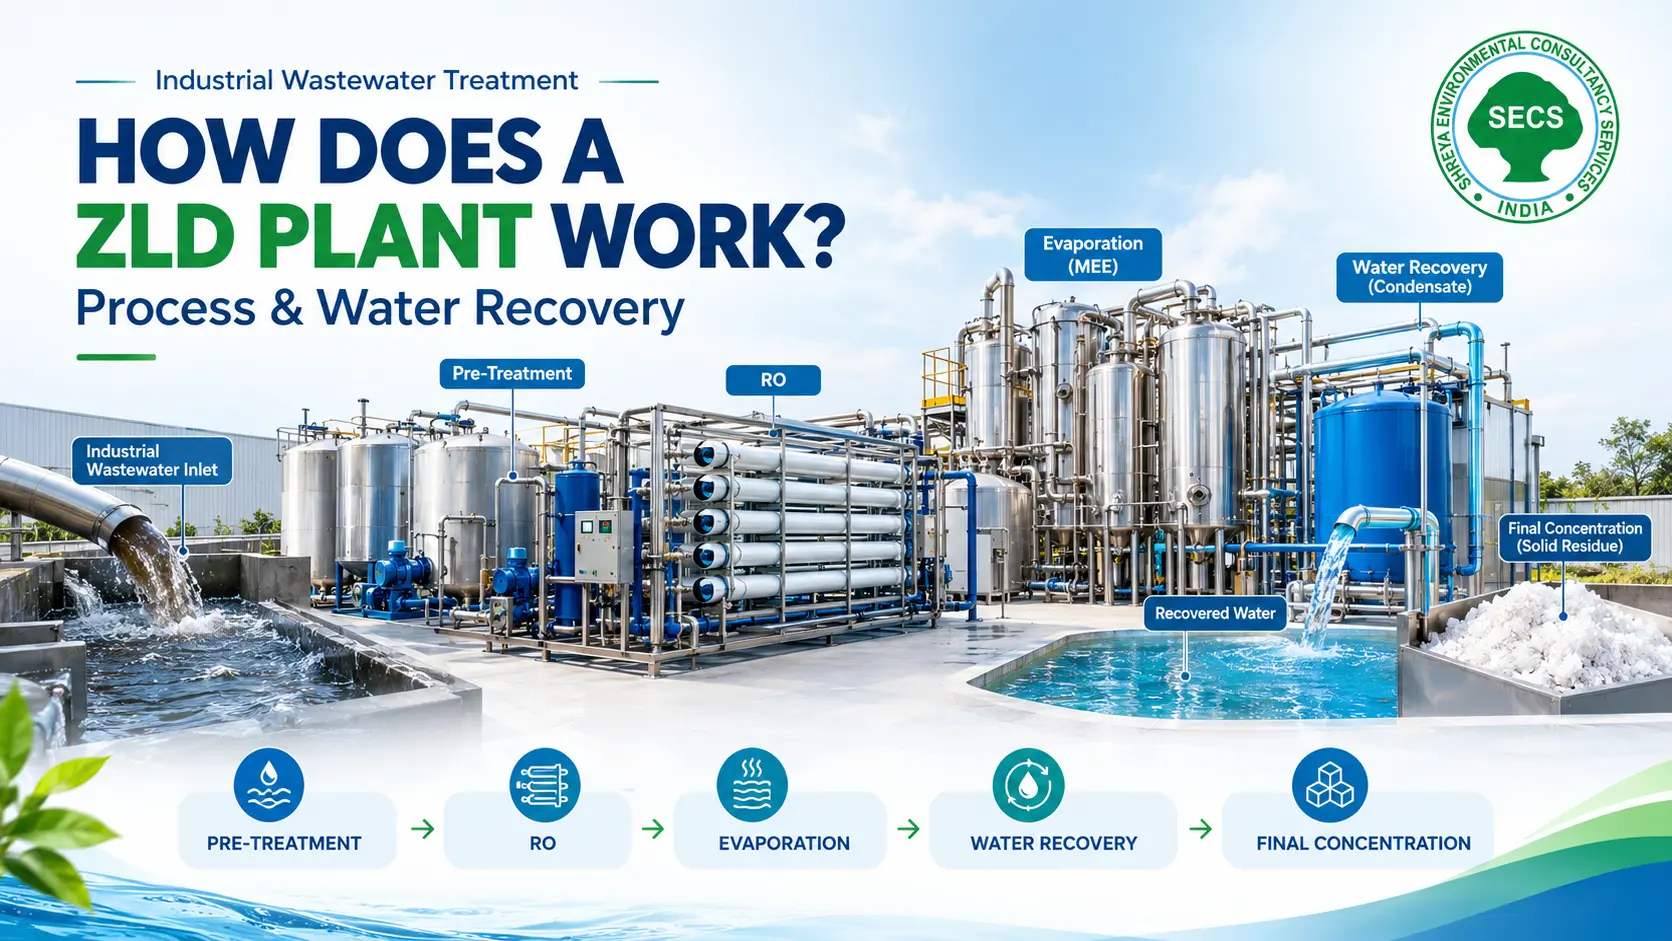
A simplified ZLD process can be represented as:
Industrial Wastewater → Pre-Treatment → RO → RO Reject → Evaporation → Concentration → Drying/Crystallization → Water Recovery and Solid Handling
The process generally begins with wastewater characterization and suitable pre-treatment. Reverse osmosis can then recover a portion of the water while concentrating dissolved salts and other contaminants into the RO reject stream.
The concentrated reject can subsequently undergo thermal treatment. During evaporation, additional water is removed as vapor and recovered as condensate, while dissolved and non-volatile components remain in the concentrated stream.
At the final stages, the concentrate may be processed through drying or crystallization to reduce the remaining liquid fraction and produce a solid or highly concentrated residue for appropriate management.
A ZLD plant is therefore not a single piece of equipment. It is a combination of treatment and recovery technologies selected according to wastewater flow, TDS, COD, hardness, scaling potential, chemical composition, energy availability, required water recovery and intended reuse of the recovered water.
Major Components of a ZLD Plant
A ZLD plant consists of multiple treatment and recovery stages working together. The exact equipment configuration depends on the characteristics of the wastewater and the treatment objectives of the facility.
1. Wastewater Collection and Equalization
Industrial wastewater is collected and, where necessary, equalized before entering the main treatment system. Equalization helps manage variations in wastewater flow and composition caused by different production cycles and operating conditions.
Wastewater characterization is an important part of the design process. Parameters such as pH, TDS, conductivity, COD, BOD, suspended solids, hardness, silica, chlorides, sulphates, oils and other industry-specific contaminants can influence the treatment configuration.
2. Pre-Treatment System
Pre-treatment prepares wastewater for downstream membrane and thermal processes. Depending on the wastewater quality, this stage may include screening, pH correction, coagulation and flocculation, clarification, filtration, softening or other specialized processes.
Effective pre-treatment can help control suspended solids, hardness, oils and other contaminants that may contribute to membrane fouling, scaling or operational problems in downstream equipment.
Where appropriate, this stage can be integrated with an existing effluent treatment plant or other industrial wastewater treatment infrastructure.
3. Reverse Osmosis System
Reverse osmosis (RO) is commonly used as an important water recovery stage in ZLD systems. Pressure is applied to force water through a semi-permeable membrane while a large proportion of dissolved salts and other contaminants remain in the concentrated reject stream.
The RO system produces two primary streams:
- RO permeate: The recovered water stream, which can be reused after achieving the quality required for its intended application.
- RO reject: The concentrated stream containing higher levels of dissolved salts and other contaminants.
Using RO before thermal treatment can reduce the volume of wastewater that needs to undergo energy-intensive evaporation.
Industries evaluating membrane-based water recovery can also consider dedicated reverse osmosis systems as part of their broader water treatment strategy.
4. Evaporator System
As RO reject becomes increasingly concentrated, further membrane treatment can become technically difficult because of increased osmotic pressure and scaling limitations. Thermal evaporation is therefore used in many ZLD configurations to remove additional water from the concentrated stream.
Depending on wastewater characteristics and project requirements, evaporator technologies may include:
- Multiple Effect Evaporator (MEE)
- Mechanical Vapor Recompression (MVR)
- Falling Film Evaporator
- Forced Circulation Evaporator
During evaporation, water is converted into vapor and subsequently condensed for recovery, while non-volatile dissolved components remain in the concentrated stream.
5. ATFD or Final Drying System
An Agitated Thin Film Dryer (ATFD) can be used for suitable highly concentrated streams where further moisture reduction is required.
The ATFD uses a heated surface and mechanical agitation to promote evaporation and reduce the moisture content of the concentrated material. Its suitability depends on factors such as solids concentration, viscosity, feed characteristics and the required final condition of the residue.
6. Crystallizer
Some ZLD systems use a crystallizer to separate dissolved salts from highly concentrated wastewater. As water is removed and the concentration of dissolved substances increases, suitable compounds can reach conditions where crystallization occurs.
The crystallization stage can therefore help convert the final concentrated liquid into a solid form that can be collected and managed appropriately.
The type and quantity of solids generated depend on the original wastewater chemistry and the selected treatment configuration.
7. Condensate and Water Recovery System
Water removed during thermal evaporation is recovered as vapor and subsequently condensed. The resulting condensate can be collected and, depending on its quality, passed through additional polishing before reuse.
The required quality of recovered water depends on its intended application. Water intended for a sensitive production or utility process may require additional treatment before reuse.
8. Solid Handling System
The final stages of ZLD can generate concentrated salts or other solid residues. These materials require appropriate collection, storage, handling and disposal arrangements based on their characteristics.
In some applications, certain materials may have potential for recovery or reuse, while other residues may require appropriate disposal according to applicable requirements.
ZLD Process Flow — Step by Step
The ZLD process flow varies according to the industry and wastewater characteristics, but the overall treatment sequence can be understood through the following stages.
Step 1: Wastewater Collection and Characterization
The process begins with collection of industrial wastewater and evaluation of its quantity and quality. Understanding the wastewater characteristics is essential before selecting treatment technologies.
Parameters such as flow, TDS, COD, hardness, silica, suspended solids, pH and specific dissolved contaminants can significantly influence process selection and equipment sizing.
Step 2: Pre-Treatment
The wastewater is conditioned to remove or reduce contaminants that could interfere with membrane or thermal treatment. Depending on the application, this may involve clarification, filtration, softening, chemical treatment or other suitable processes.
The objective is to provide a more suitable feed for the downstream recovery stages.
Step 3: RO Water Recovery
The pre-treated wastewater enters the reverse osmosis system. Water passes through the membrane as permeate while dissolved salts and other contaminants become concentrated in the RO reject.
This stage allows a portion of the suitable water to be recovered before the concentrated stream moves toward thermal treatment.
Step 4: RO Reject Moves to Concentration
The RO reject contains a higher concentration of dissolved substances and therefore requires further treatment in a ZLD system.
Instead of releasing the reject as a liquid waste stream, it is generally directed toward additional concentration and separation stages.
Step 5: Thermal Evaporation
The concentrated RO reject enters an evaporator where additional water is removed through thermal evaporation. The generated vapor can be condensed and collected as recovered water.
The remaining stream becomes progressively more concentrated as water is removed.
Step 6: Further Concentration
As evaporation continues, dissolved salts and other non-volatile components remain in the concentrate. The concentration increases until the stream reaches the conditions required for the final separation stage.
Operating conditions depend on wastewater chemistry, scaling behaviour, solids concentration and the selected equipment configuration.
Step 7: Drying or Crystallization
The highly concentrated stream can then undergo ATFD treatment, crystallization or another suitable final separation process.
This stage reduces the remaining moisture and converts the final concentrate into a manageable solid or semi-solid residue, depending on the process configuration.
Step 8: Water Recovery and Reuse
Water recovered through RO and thermal treatment can potentially be reused within the industrial facility after achieving the required quality for the intended application.
Depending on the reuse requirement, recovered water may require additional polishing or treatment before being returned to production processes, utility systems or other suitable applications.
How Does a ZLD Plant Recover Water?
ZLD water recovery takes place through multiple treatment stages rather than through a single piece of equipment.
The first major recovery stage is often reverse osmosis, where water passes through a semi-permeable membrane while a significant portion of dissolved contaminants remains in the reject stream.
Additional water recovery takes place during evaporation. Water contained in the concentrated reject is converted into vapor, condensed and collected as condensate.
The total recovery achieved by a ZLD system depends on wastewater characteristics, membrane recovery, scaling limitations, thermal system design, operating conditions and the required final water quality.
For this reason, a specific recovery percentage should not be assumed for every ZLD plant. Actual process design should be based on wastewater analysis and the intended reuse requirements.
What Happens to RO Reject in a ZLD Plant?
RO reject is one of the most important streams in a ZLD process because it contains a higher concentration of dissolved salts and other contaminants than the original RO feed.
In a conventional RO application, reject may require separate disposal or additional treatment. In a ZLD system, the reject is generally directed toward additional concentration stages.
The reject can enter an evaporator where additional water is removed. The resulting concentrate may then undergo further treatment through ATFD, crystallization or another suitable final separation process.
This allows the system to recover additional water while progressively concentrating the remaining dissolved material rather than leaving it as a final liquid discharge.
Technologies Used in ZLD
A ZLD system can combine several technologies depending on the wastewater characteristics, recovery requirements and operating conditions of the facility.
- Reverse Osmosis (RO): Used for membrane-based water recovery and reduction of the volume entering thermal treatment.
- Multiple Effect Evaporator (MEE): Used for thermal concentration of suitable high-TDS streams.
- Mechanical Vapor Recompression (MVR): Uses mechanical vapor recompression to support evaporation and may be considered where energy efficiency is an important design factor.
- Falling Film Evaporator: Used for evaporation of suitable wastewater streams with appropriate feed characteristics.
- Forced Circulation Evaporator: Suitable for certain concentrated streams where circulation and heat-transfer conditions require a different evaporator configuration.
- ATFD: Used for further concentration and drying of suitable concentrated streams.
- Crystallizer: Used in suitable applications to promote crystallization and separation of dissolved solids.
The final combination should be selected according to actual wastewater chemistry, flow rate, recovery objectives, energy availability, scaling potential and operating requirements.
Factors Affecting ZLD Plant Design
A reliable ZLD system begins with understanding the wastewater rather than selecting equipment first. Several factors can influence the final process configuration.
- Wastewater flow: Determines treatment capacity and equipment sizing.
- TDS and conductivity: Influence membrane recovery and thermal concentration requirements.
- Hardness and scaling potential: Can affect membranes, heat-transfer surfaces and evaporator operation.
- COD and organic load: Can influence pre-treatment requirements and membrane performance.
- Silica and dissolved salts: Certain constituents can create scaling or crystallization challenges.
- Suspended solids and oils: May require effective pre-treatment before membrane treatment.
- Required water recovery: Higher recovery objectives can require additional treatment stages.
- Final water quality: Determines the level of polishing required before reuse.
- Energy availability: Thermal treatment can have significant energy requirements.
- Final residue: The quantity and characteristics of concentrated solids affect handling and disposal.
These factors demonstrate why a ZLD plant should be engineered specifically for the wastewater and operating conditions of the individual facility.
Benefits and Considerations of ZLD
When appropriately designed and operated, a ZLD system can provide several benefits for industrial wastewater management.
- Recovery and reuse of suitable wastewater streams
- Reduction or elimination of final liquid wastewater discharge
- Better management of high-TDS RO reject
- Reduced dependence on freshwater for suitable industrial applications
- Integration with existing ETP and RO infrastructure
- Controlled concentration and management of dissolved solids
- Potential recovery of certain salts or materials in suitable applications
- Improved control over complex industrial wastewater streams
However, ZLD also requires careful engineering and operation. Thermal treatment can involve substantial energy consumption, while scaling, fouling, corrosion and solid handling can affect operating performance.
The objective should therefore be to develop the appropriate combination of treatment technologies for the specific wastewater rather than simply adding more treatment stages.
ZLD Applications for Industries in Baddi
ZLD in Baddi can be relevant for industrial facilities that need advanced management of high-TDS wastewater, RO reject and water recovery requirements. Different manufacturing operations can generate wastewater with significantly different chemical characteristics, flow rates and treatment challenges.
Industries such as pharmaceutical manufacturing, chemical processing, food and beverage production, textiles and other manufacturing operations may have different wastewater treatment requirements. As a result, the ZLD process should be evaluated according to the specific industrial wastewater rather than using a standard configuration for every facility.
A ZLD plant in Baddi may be considered where water recovery, concentrated wastewater management and reduction of liquid discharge are important parts of the facility's water management strategy.
Before finalizing a system, factors such as wastewater composition, TDS, COD, hardness, scaling potential, flow rate, recovery objectives, energy availability and intended water reuse should be evaluated.
For facilities requiring a broader wastewater treatment setup, ZLD can also be integrated with existing ETP and STP technologies and other treatment processes.
Frequently Asked Questions About ZLD Plants
How does a ZLD plant work?
A ZLD plant progressively treats and concentrates industrial wastewater through stages such as pre-treatment, reverse osmosis, evaporation and final drying or crystallization. Water is recovered during membrane and thermal treatment while the remaining dissolved solids are concentrated for appropriate final management.
What are the main components of a ZLD plant?
Common components can include wastewater pre-treatment, reverse osmosis, evaporators such as MEE or MVR systems, ATFD or other drying equipment, crystallizers, condensate recovery systems and solid handling equipment. The exact combination depends on wastewater characteristics and project requirements.
What happens to RO reject in ZLD?
RO reject is generally sent to downstream concentration stages instead of being discharged as liquid wastewater. Depending on the process configuration, it can undergo evaporation followed by further drying or crystallization so that additional water is recovered and the remaining solids can be managed.
How does a ZLD plant recover water?
Water is recovered through multiple stages. Reverse osmosis produces permeate, while thermal evaporation produces condensate. Depending on the required quality, these recovered water streams may undergo additional polishing before reuse.
What is MEE in a ZLD plant?
MEE stands for Multiple Effect Evaporator. It is a thermal evaporation system used to remove water from concentrated wastewater. In a multiple-effect arrangement, vapor generated in one effect can provide heating energy for another effect, depending on the system design.
What is the role of ATFD in ZLD?
ATFD stands for Agitated Thin Film Dryer. It can be used to further concentrate and dry suitable high-TDS streams after upstream treatment and evaporation. Its suitability depends on feed characteristics, solids concentration, viscosity and the required final residue condition.
Does every ZLD plant use the same process?
No. The configuration of a ZLD plant varies according to wastewater flow, TDS, COD, hardness, scaling potential, chemical composition, recovery requirements, energy availability and final water quality requirements. Process selection should therefore be based on actual wastewater characteristics.
Is ZLD available in Baddi for industrial wastewater treatment?
Yes, industries in Baddi can implement ZLD systems for recovering water from concentrated wastewater and managing high-TDS streams with minimal or no final liquid discharge. The appropriate ZLD configuration depends on wastewater characteristics, treatment capacity, recovery requirements and the specific process conditions of each industrial facility.
Can ZLD be integrated with an existing ETP or RO system?
Yes. Depending on the wastewater characteristics and existing infrastructure, a ZLD system can be integrated with an existing ETP, RO system or other wastewater treatment processes. The existing system should be evaluated to determine whether its capacity, treated-water quality and operating conditions are suitable for integration with the proposed ZLD process.
How Shreya Environmental Consultancy Services Can Help With Your ZLD Project
A successful ZLD project requires more than installing an evaporator or adding a final treatment stage. The overall system needs to be evaluated as an integrated wastewater treatment process, from wastewater characterization and pre-treatment through water recovery and final residue management.
Shreya Environmental Consultancy Services can support industries in evaluating and developing wastewater treatment solutions according to their specific project requirements. The approach can include assessment of wastewater characteristics, treatment requirements, recovery objectives and integration with existing treatment infrastructure.
Depending on the application, the ZLD system can be planned alongside an effluent treatment plant, reverse osmosis system or other treatment technologies to create a more integrated wastewater management solution.
Shreya also provides broader water and wastewater treatment solutions for industrial applications, allowing different treatment requirements to be considered as part of the overall project rather than as isolated systems.
Where environmental planning and regulatory requirements form part of the project, environmental consultancy services can also support the wider environmental management approach.
The appropriate ZLD configuration ultimately depends on the individual facility. Wastewater analysis, process selection, equipment sizing, water recovery requirements and final residue management should all be considered before implementation.
Conclusion
A ZLD plant works by progressively treating, concentrating and separating industrial wastewater so that water can be recovered while the remaining dissolved solids are managed as concentrated or solid residue. Depending on the wastewater characteristics, the process may combine pre-treatment, reverse osmosis, evaporation, concentration, ATFD, crystallization and condensate recovery.
The most important part of ZLD plant design is selecting the right combination of technologies for the specific wastewater. Flow rate, TDS, COD, hardness, scaling potential, energy requirements, recovery objectives and final water quality all influence the final process configuration.
For industries considering ZLD in Baddi, a site-specific wastewater assessment can help establish the appropriate process flow, water recovery strategy and final residue management approach. Shreya Environmental Consultancy Services works across industrial water and wastewater treatment applications, including ZLD, RO, ETP and environmental consultancy, helping industries evaluate treatment solutions according to their project requirements.